

Strong flavour colour coding
Pink, orange, brown, blue, tan and green fields provide fast visual differentiation across the range while allowing every pouch to remain recognizable as Haley’s Pantry.
Real Packaging Case Study
A coordinated family of brightly colour-coded granola snack pouches that keeps the master brand and product architecture consistent while differentiating numerous flavours.
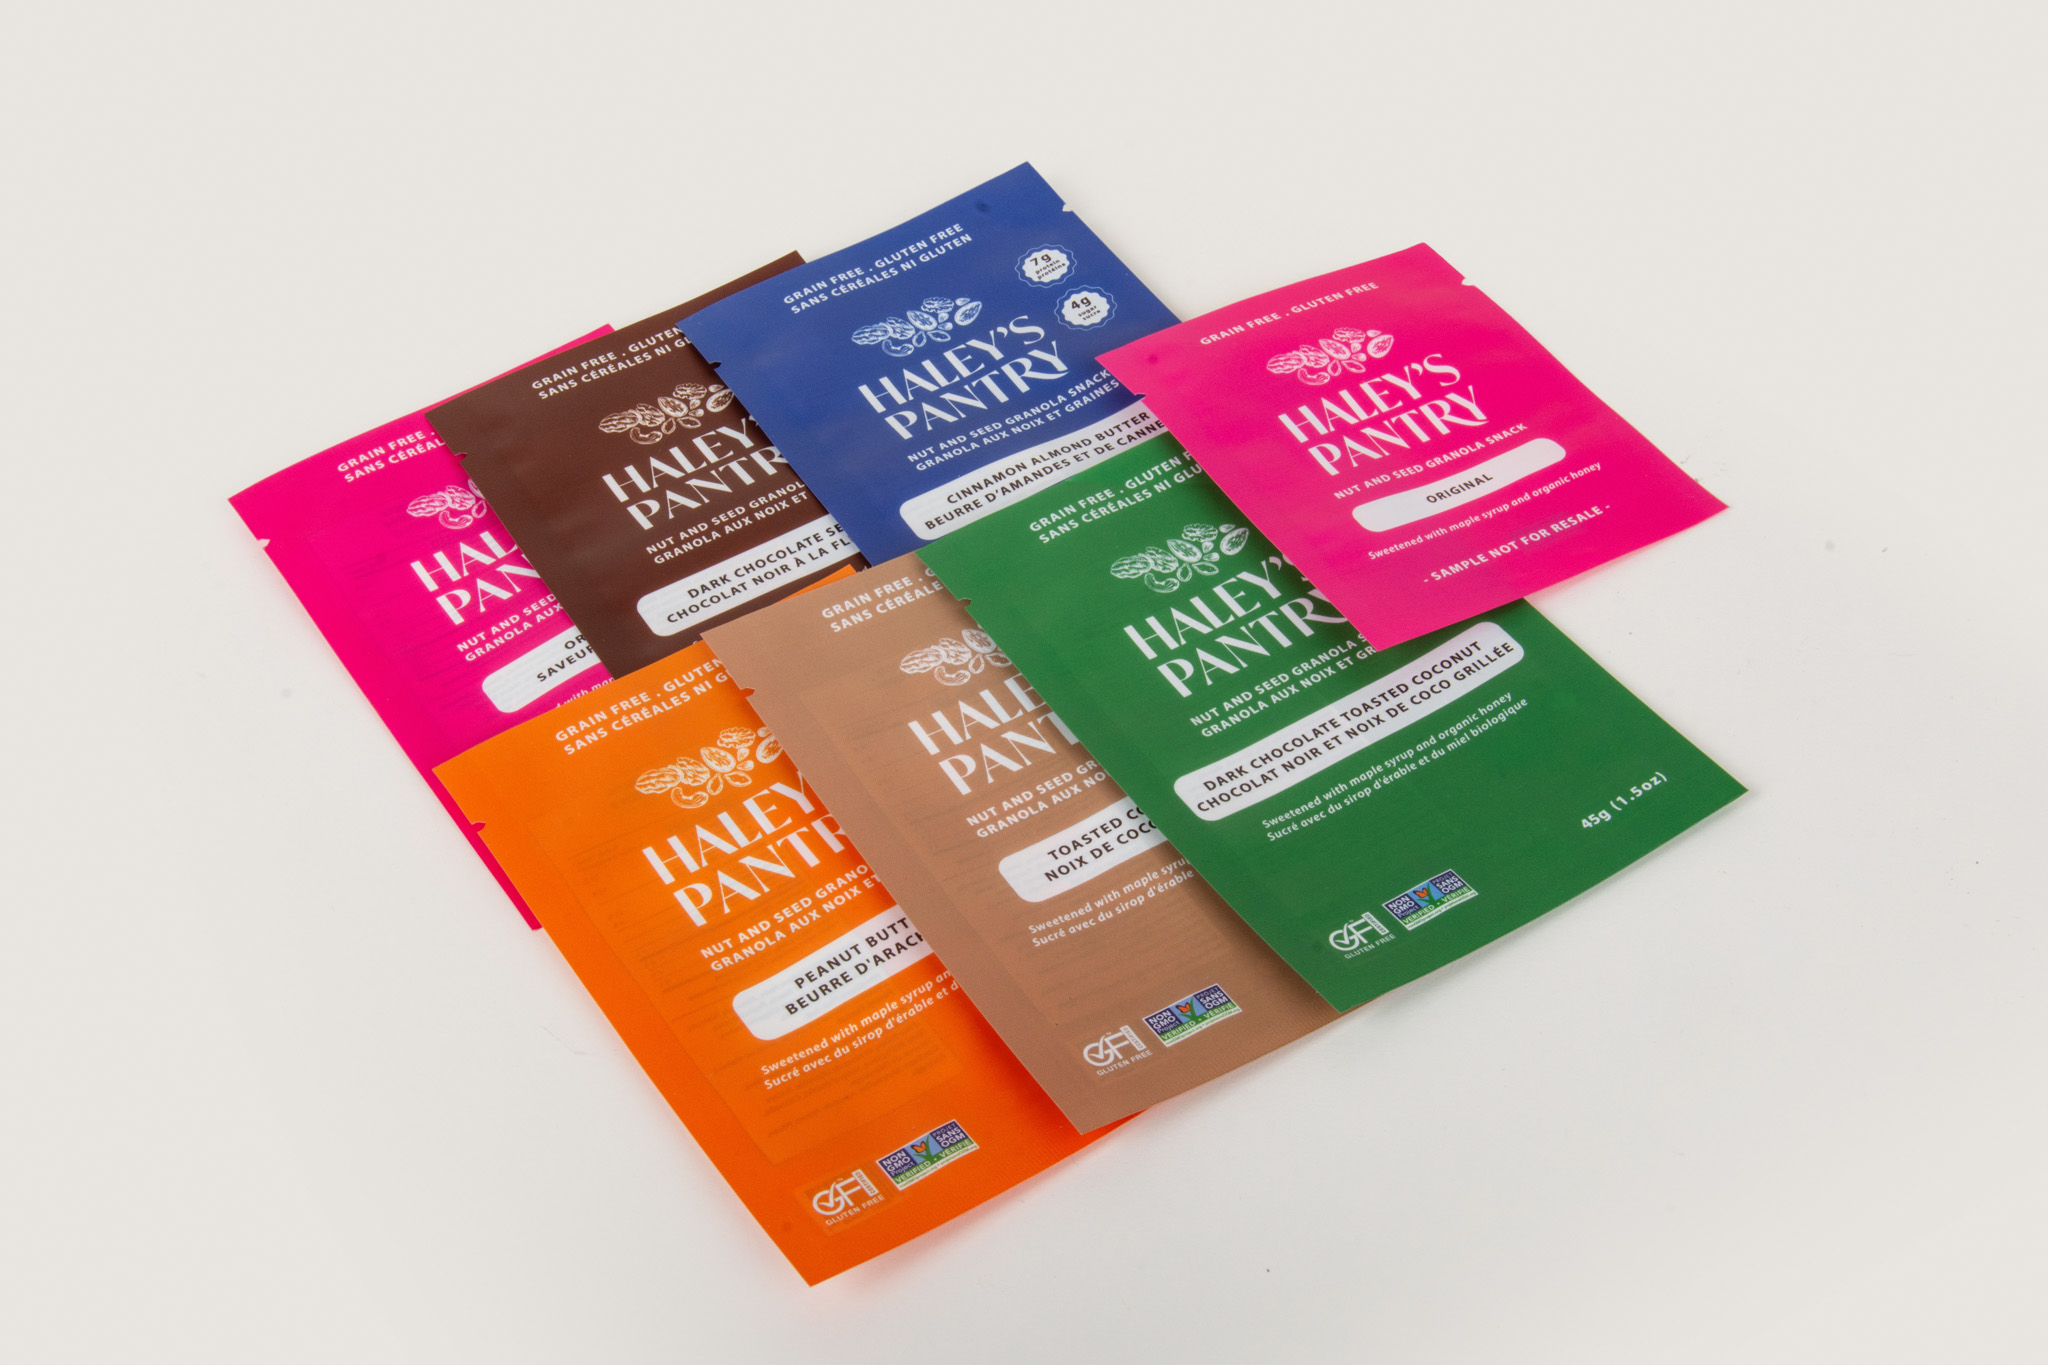
A product line with many flavours needs each SKU to be easy to distinguish without weakening the master brand. The packaging keeps the logo, hierarchy, white flavour panel and certification area in repeatable positions while assigning a strong colour to each variety.
Pink, orange, brown, blue, tan and green fields provide fast visual differentiation across the range while allowing every pouch to remain recognizable as Haley’s Pantry.
The grain-free and gluten-free line, master brand, product category and flavour name appear in a consistent top-to-bottom sequence across the visible designs.
A white rounded rectangle isolates each flavour name from its background colour, supporting legibility even when the palette changes dramatically between SKUs.
Certification marks and net weight remain grouped near the lower edge, helping prevent product claims and verification marks from competing with the primary brand message.
When several flavours share similar product names and pack sizes, subtle differences can be missed. Large background colour changes give each variety a clear visual identity.
The design changes the dominant colour and flavour name while preserving structure and hierarchy. This balances recognition of the family with quick flavour selection.
The pack needs to present product type, dietary positioning, flavour, sweetener statement and certification marks without becoming visually disorganized.
Claims are assigned to predictable zones, leaving the brand and flavour as the strongest elements and supporting scanning across a retail display.
A production quotation should confirm pouch dimensions, product fill, required barrier and seal performance, material structure, printing coverage, closure format, pack testing, order quantity and destination. The appropriate packaging specification must be validated for the food product and intended shelf life. Beneco’s standard minimum order quantity is 5,000 units.
Documentation note: This case describes visible printed designs in the supplied photograph. The precise pouch structure, film layers, barrier properties, sealing method, dimensions, production quantity and measured results are not inferred.
Prepared byBeneco Packaging Technical Editorial Team
ReviewedAugust 24, 2026 · Editorial Policy
Share your product, flavour count, pouch specifications, artwork, quantity and delivery requirements with Beneco.